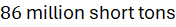 ) by 2050. Standard crystalline silicon (c-Si) photovoltaic modules are engineered for multi-decade operational durability (
 to
 years), comprising a tightly bonded multi-layer laminate structure featuring tempered low-iron front glass, cross-linked ethylene vinyl acetate (EVA) encapsulant, monocrystalline or multicrystalline silicon wafers, silver metallization grid lines, and polymeric backsheets. Recovering valuable semiconductor-grade materials from this robust composite requires precise thermal delamination, mechanical separation, and chemical etching processes to prevent material degradation and environmental contamination.
Thermal Delamination and Encapsulant Decomposition Physics
The primary structural challenge in photovoltaic panel recycling is separating the laminated components without fracturing the ultra-thin silicon wafers ( to
 in thickness). The front glass and silicon wafer layers are permanently bonded together using ethylene vinyl acetate (EVA) copolymer resins subjected to high-temperature vacuum lamination during manufacturing. EVA undergoes peroxide-initiated cross-linking, forming a three-dimensional thermoset polymer network that resists mechanical peeling.
To break down this thermoset polymer matrix, industrial recycling plants utilize thermal delamination furnaces operating at temperatures between  and
 (
 to
 ). Under these thermal conditions, the EVA encapsulant undergoes thermal pyrolysis and oxidative degradation:
- Polymer Scission: Covalent carbon-carbon and ester bonds within the EVA molecular chains undergo thermal cracking, releasing volatile organic compounds, acetic acid vapor, and non-condensable hydrocarbon gases.
- Char Combustion: Controlled oxygen injection within the secondary combustion zone oxidizes residual organic char from the glass and wafer surfaces, leaving clean, delaminated components.
- Off-Gas Scrubbing: Pyrolysis off-gases are routed through catalytic thermal oxidizers and wet alkaline scrubbers to neutralize hazardous acid gases (such as acetic acid and trace fluorine compounds) before atmospheric release.
While thermal delamination is efficient, temperature profiles must be strictly controlled to prevent localized thermal runaways or wafer warping.
Mechanical Demolition and Glass Separation
Prior to thermal processing, automated mechanical pre-treatment strips non-semiconductor peripheral components to streamline downstream recycling efficiency. Hydraulic shears and automated clamping mechanisms remove the anodized aluminum frame encircling the module perimeter, while automated routing tools excise the waterproof junction box containing copper wiring and bypass diodes.
Following frame removal, the bare glass-laminate panel enters specialized crushing and roller-separation machinery. The tempered front glass—accounting for approximately 70% to 75% of total module mass—is fractured and separated from the underlying encapsulant and cell matrix. Mechanical shaking tables and pneumatic air classifiers segregate clean, high-purity glass cullet suitable for direct secondary use in fiberglass manufacturing or flat glass production, eliminating silica waste streams.
Silicon Wafer Chemical Etching and Silver Recovery
Once delaminated and cleaned of residual encapsulant polymers, the recovered silicon wafers retain front-side silver busbars, rear-side aluminum metallization layers, and an anti-reflective silicon nitride ( ) coating. Reclaiming high-purity silicon and precious metals requires targeted chemical etching and hydrometallurgical separation.
Chemical etching utilizes multi-stage acid baths to dissolve metallic contacts and surface coatings selectively:
- Aluminum Removal: Wafers are immersed in dilute sodium hydroxide (
 ) or hydrochloric acid (
 ) solutions to dissolve the rear aluminum back-surface field.
- Anti-Reflective Coating Stripping: Hydrofluoric acid (HF) etching removes the
 anti-reflective dielectric layer without eroding the underlying silicon substrate.
- Silver Metallization Recovery: Silver grid lines are dissolved using specialized oxidizing acid mixtures (such as nitric acid
 combined with hydrogen peroxide), followed by electrolytic or chemical precipitation to recover high-purity silver powder.
Technical Data Specifications of Photovoltaic Recycling Parameters
| Recycling & Material Parameter | Engineering Specification Range |
|---|---|
| Thermal Delamination Temperature |  to  (  to  ) |
| Silicon Wafer Thickness |  to  nominal profile |
| Recovered Glass Purity |  cullet purity for secondary manufacturing |
| Silver Recovery Efficiency | 90% to 98% precious metal reclamation rate |
| Silicon Wafer Recovery Yield | 80% to 90% whole or crack-free wafer yield |
Acid Leaching Concentration ( ) |  to  silver dissolution bath |
| Embodied Energy Reduction | 70% to 85% energy savings vs. virgin silicon production |
Silicon Purity Refinement and Solar-Grade Upcycling
Recovered silicon wafers frequently retain minor surface impurities, trace metal dopants (boron or phosphorus), and structural micro-defects induced by initial manufacturing and mechanical delamination. Utilizing recovered silicon for new photovoltaic cell production requires chemical refinement to achieve solar-grade purity standards (99.9999% or 6N purity).
Refinement proceeds via chemical mechanical polishing (CMP) to remove surface sawing damage, followed by directional solidification or advanced acid leaching. Cleaned silicon is re-melted in induction furnaces and subjected to Czochralski crystal growth pulling processes or cast into new multicrystalline ingots. Re-melting recovered silicon consumes significantly less energy than reducing raw quartz sand ( ) via the traditional carbon-reduction Siemens process (
 or
 ).
Life-Cycle Assessments and Circular Economy Realities
Quantitative life-cycle assessments (LCAs) published by the UNEP, IEA, and academic clean-tech research consortia confirm that closed-loop photovoltaic panel recycling reduces cumulative energy demand and greenhouse gas emissions by up to 80% compared to virgin material extraction. As national regulatory bodies implement mandatory extended producer responsibility (EPR) frameworks and minimum recycled content standards for solar installations, scalable recycling technologies eliminate landfill accumulation. By establishing closed-loop recovery pathways for silicon wafers, silver, and structural glass, photovoltaic recycling decouples renewable energy expansion from virgin mineral depletion.
Comments (0)
Login to leave a comment.
No comments yet. Be the first to share your thoughts!