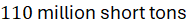 ) annually, while less than 15% of post-consumer garments undergo recycling. Traditional mechanical recycling degrades fiber tensile strength by shortening polymer chains through aggressive shredding. In contrast, chemical depolymerization, enzymatic hydrolysis, and solvent-based dissolution restore post-consumer blended textiles into virgin-grade polymers without mechanical degradation. Executing scalable closed-loop garment recycling requires precise control over chemical depolymerization kinetics, solvent recovery systems, and multi-component fiber separation.
Polymer Blends and the Mechanical Recycling Bottleneck
Post-consumer textile waste consists overwhelmingly of complex blended fabrics—most commonly polyester-cotton ( ) blends. Mechanical recycling is fundamentally unequipped to process these heterogeneous mixtures. When blended textiles pass through mechanical shredders and carding machines, synthetic polyester fibers and natural cellulose fibers interlock physically, producing weak, low-grade insulation or industrial padding.
Chemical recycling bypasses this physical limitation by dissolving or chemically cleaving specific polymer structures within the blend while leaving other components unaffected. For example, treating a  blend with targeted chemical reagents dissolves the polyester matrix into liquid monomers while preserving insoluble cellulose fibers, or conversely, dissolves cellulose while leaving polyester strands intact. This selective chemical fractionation enables complete separation of complex blended garments into pure, single-stream raw materials.
Polyester Depolymerization: Glycolysis and Methanolysis
Polyethylene terephthalate ( ) accounts for over 50% of global fiber production. Chemical recycling of waste polyester relies primarily on thermochemical depolymerization routes—glycolysis, methanolysis, and hydrolysis—which break long ester linkages in the polymer backbone down into constituent monomers.
- Glycolysis: Waste polyester fabric is treated with excess ethylene glycol (
 ) at elevated temperatures between
 and
 (
 to
 ) under pressure in the presence of transesterification catalysts (such as zinc acetate or manganese acetate). This reaction cleaves polymer chains to produce bis(2-hydroxyethyl) terephthalate (BHET), an intermediate monomer that is subsequently repolymerized into virgin-grade PET.
- Methanolysis: Depolymerizes waste PET using superheated methanol (
 ) vapor at temperatures between
 and
 (
 to
 ) and pressures up to
 (
 ). Methanolysis yields dimethyl terephthalate (DMT) and ethylene glycol, which undergo fractional distillation to remove impurities and dyes before re-synthesis.
- Hydrolysis: Utilizes acidic, alkaline, or enzymatic catalysts in aqueous solutions to break ester bonds, directly yielding pure terephthalic acid (TPA) and ethylene glycol.
These chemical degradation routes eliminate thermal history degradation, producing recycled monomers chemically indistinguishable from petroleum-derived virgin feedstocks.
Cellulosic Dissolution and Enzymatic Hydrolysis
Natural cellulosic fibers—such as cotton, viscose, and modal—dominate the other half of the global textile market. Chemical recycling of post-consumer cotton requires breaking down crystalline cellulose macromolecular structures without destroying the glucose monomer chains.
Solvent-based dissolution technologies utilize ionic liquids, N-methylmorpholine N-oxide (NMMO), or direct carbamation processes to dissolve cellulose waste directly into a viscous dope solution. Once filtered and extruded through spinnerets into a coagulation bath, regenerated cellulose fibers (such as lyocell or new-generation man-made cellulosic fibers) emerge with high tensile strength and moisture absorption properties.
Alternatively, enzymatic hydrolysis utilizes specialized cellulase enzyme complexes produced by genetically engineered fungi (such as Trichoderma reesei). Cellulase enzymes target  -1,4-glycosidic bonds linking glucose units within the cellulose chain, hydrolyzing waste cotton garments down into pure glucose syrups. These glucose monomers subsequently serve as biological feedstocks for bacterial fermentation into PHA bioplastics or ethanol, establishing cross-industry circularity.
Technical Data Specifications of Textile Recycling Parameters
| Processing Technology | Target Fiber Input | Operating Conditions | Primary Output Product |
|---|---|---|---|
| PET Glycolysis | Polyester ( ) |  to  (  to  ); catalyzed | BHET monomer for repolymerization |
| PET Methanolysis | Polyester ( ) |  to  (  to  );  | Purified DMT and ethylene glycol |
| Ionic Liquid Dissolution | Cotton / Cellulosics |  to  (  to  ); solvent bath | Regenerated cellulose fibers |
| Enzymatic Hydrolysis | Post-consumer cotton |  (  ); pH 4.8 aqueous reactor | Glucose monomers for fermentation |
| Selective Fractionation |  blends | Multi-stage solvent separation loops | Pure isolated polyester & cellulose streams |
Solvent Recovery Systems and Chemical Loop Efficiency
The economic viability and environmental sustainability of textile waste chemical recycling depend strictly on closed-loop solvent recovery efficiency. Industrial chemical recycling facilities deploy multi-stage fractional distillation columns, vacuum evaporation units, and membrane filtration systems to capture and purify reactive solvents (such as ethylene glycol, methanol, and ionic liquids) with recovery rates exceeding 99%.
Minimizing makeup chemical additions reduces operating expenditures and prevents toxic chemical discharge into municipal wastewater streams. Furthermore, life-cycle assessments published by academic research consortia indicate that closed-loop chemical recycling of synthetic and cellulosic textiles reduces greenhouse gas emissions by 40% to 70% compared to virgin petrochemical and conventional agricultural cotton production. By scaling chemical depolymerization infrastructure, the global textile industry eliminates landfill accumulation and establishes true circular material flows.
Comments (0)
Login to leave a comment.
No comments yet. Be the first to share your thoughts!